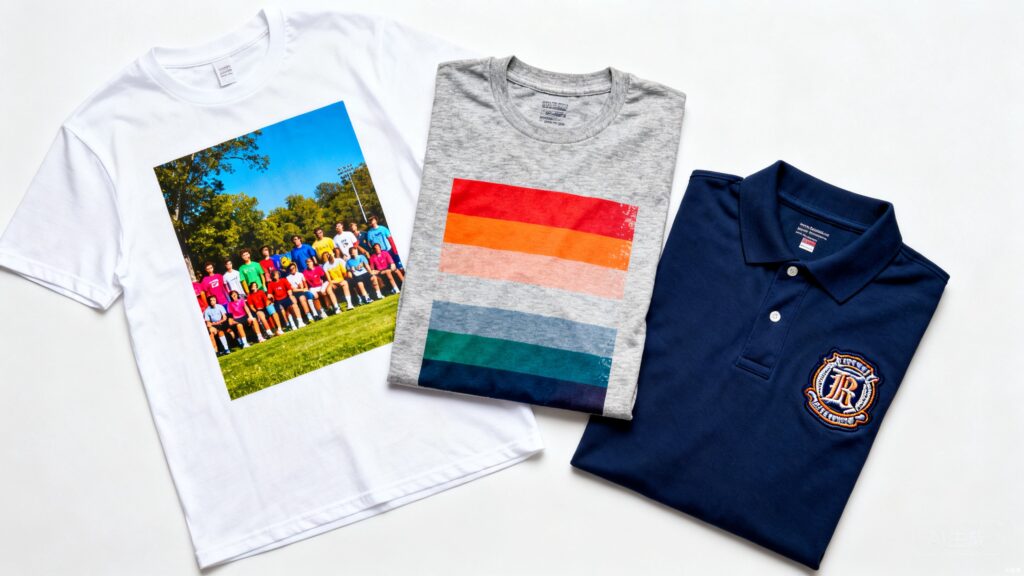
If you’ve ever wondered whether to use sublimation, screen printing or embroidery for your custom t-shirts, you’re not alone. The three methods look similar from the outside, but they behave completely differently once you factor in fabric type, design complexity, order quantity and budget.
At OEM T-Shirts we produce all three every day at our Yiwu factory, so this guide is written from the production floor, not from a marketing deck. By the end you’ll know exactly which method fits your next project — and how to request a quote in the format our production team needs to get you a fast, accurate price.
Quick verdict: which method when?
Before we get into the long answer, here’s the cheat sheet our sales team uses internally:
- Full-color design + white or light polyester blank? → Sublimation. Best vibrancy, no setup fee, MOQ 25.
- Bold 1–4 color logo + cotton t-shirt? → Screen printing. Cheapest at 50+ pieces, most durable plastisol finish.
- Premium polo, workwear or corporate logo on chest? → Embroidery. Most professional, lasts the life of the garment.
- One-off sample or photo-realistic print on cotton? → DTG. No screens, full color, but slower.
Now let’s look at why.
What is sublimation printing?
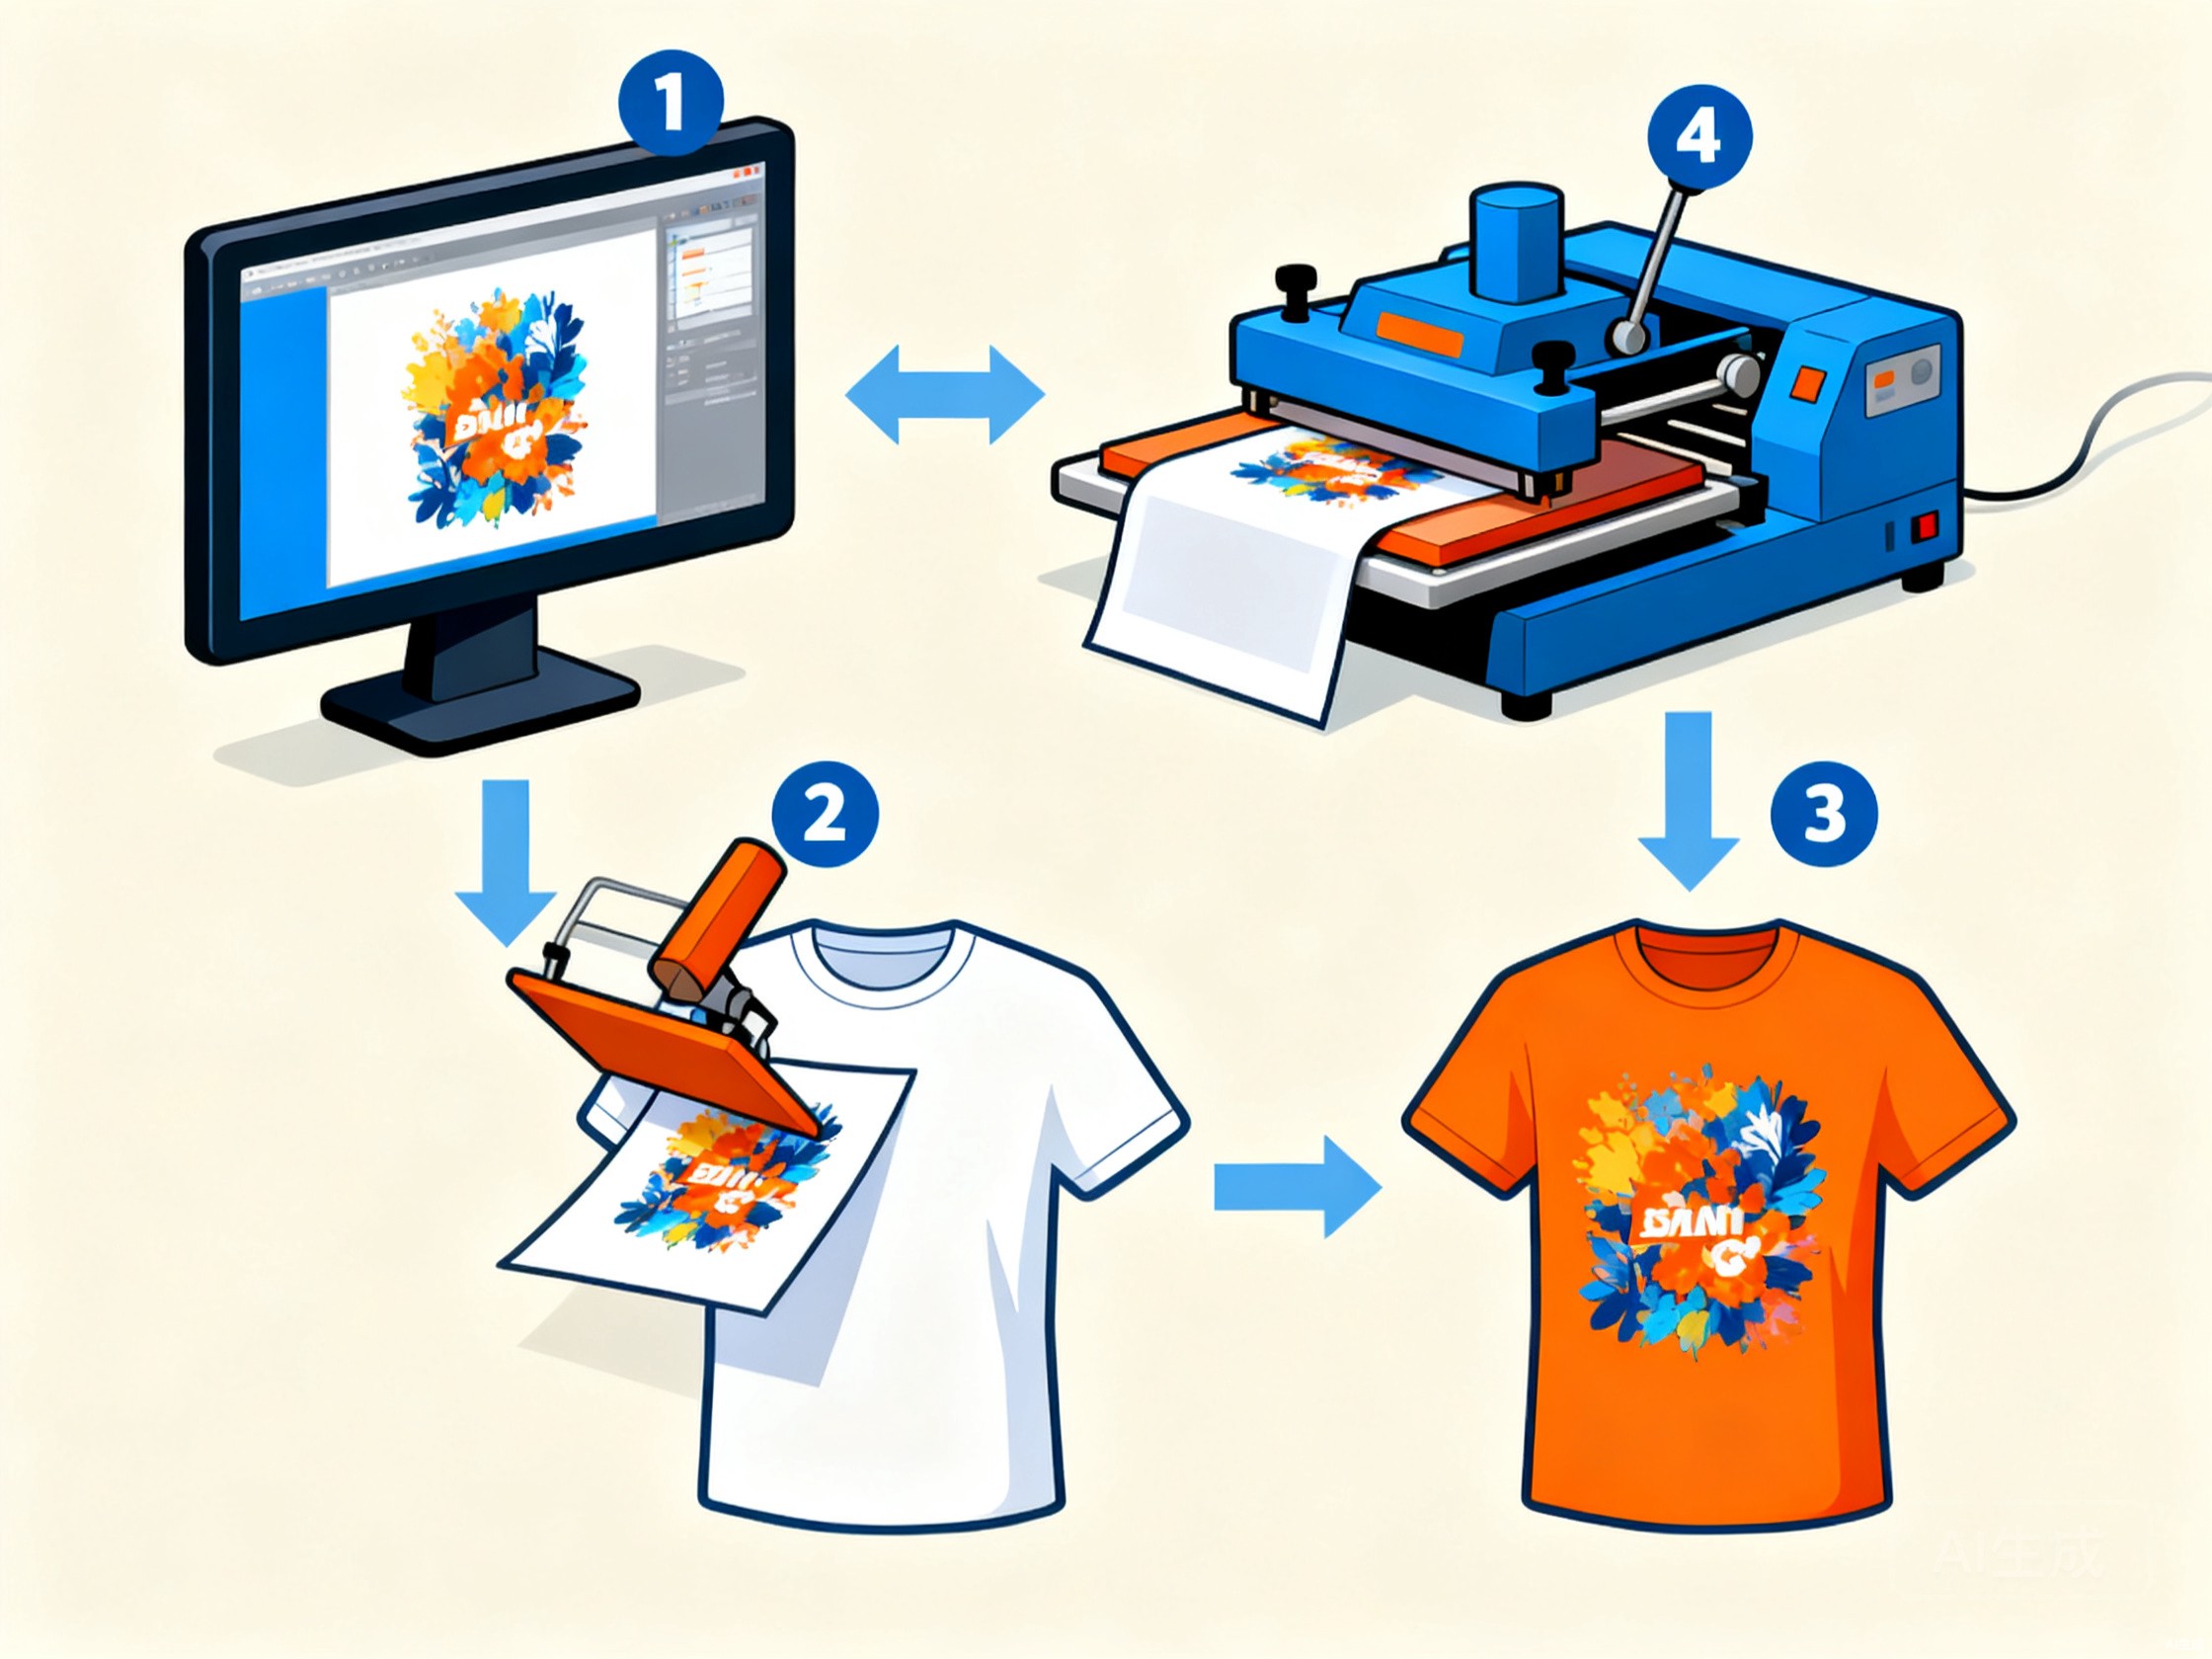
Sublimation printing uses heat (around 200 °C / 400 °F) and pressure to turn solid dye into gas that bonds directly with polyester fibers. The dye becomes part of the fabric — there is no ink layer sitting on top. The result feels soft, has no texture and does not crack, peel or fade even after 50+ washes.
When sublimation wins
- Photographic, full-color artwork with gradients, shadows and skin tones
- All-over prints that wrap from front to back and side to side
- Small-batch orders (MOQ 25) because there are no screens to set up
- Light or white polyester blanks
When sublimation is the wrong choice
- 100% cotton blanks — the dye has nothing to bond with
- Dark fabric — white ink underbase is required, which adds cost and texture
- Single-color logos where screen printing would be 3× cheaper
Pro tip: If your design has both photo and text elements, ask us about sublimation + embroidery hybrids — the photo body gets sublimated and your logo gets stitched on top. It’s a popular combo on our custom polo line.
What is screen printing?
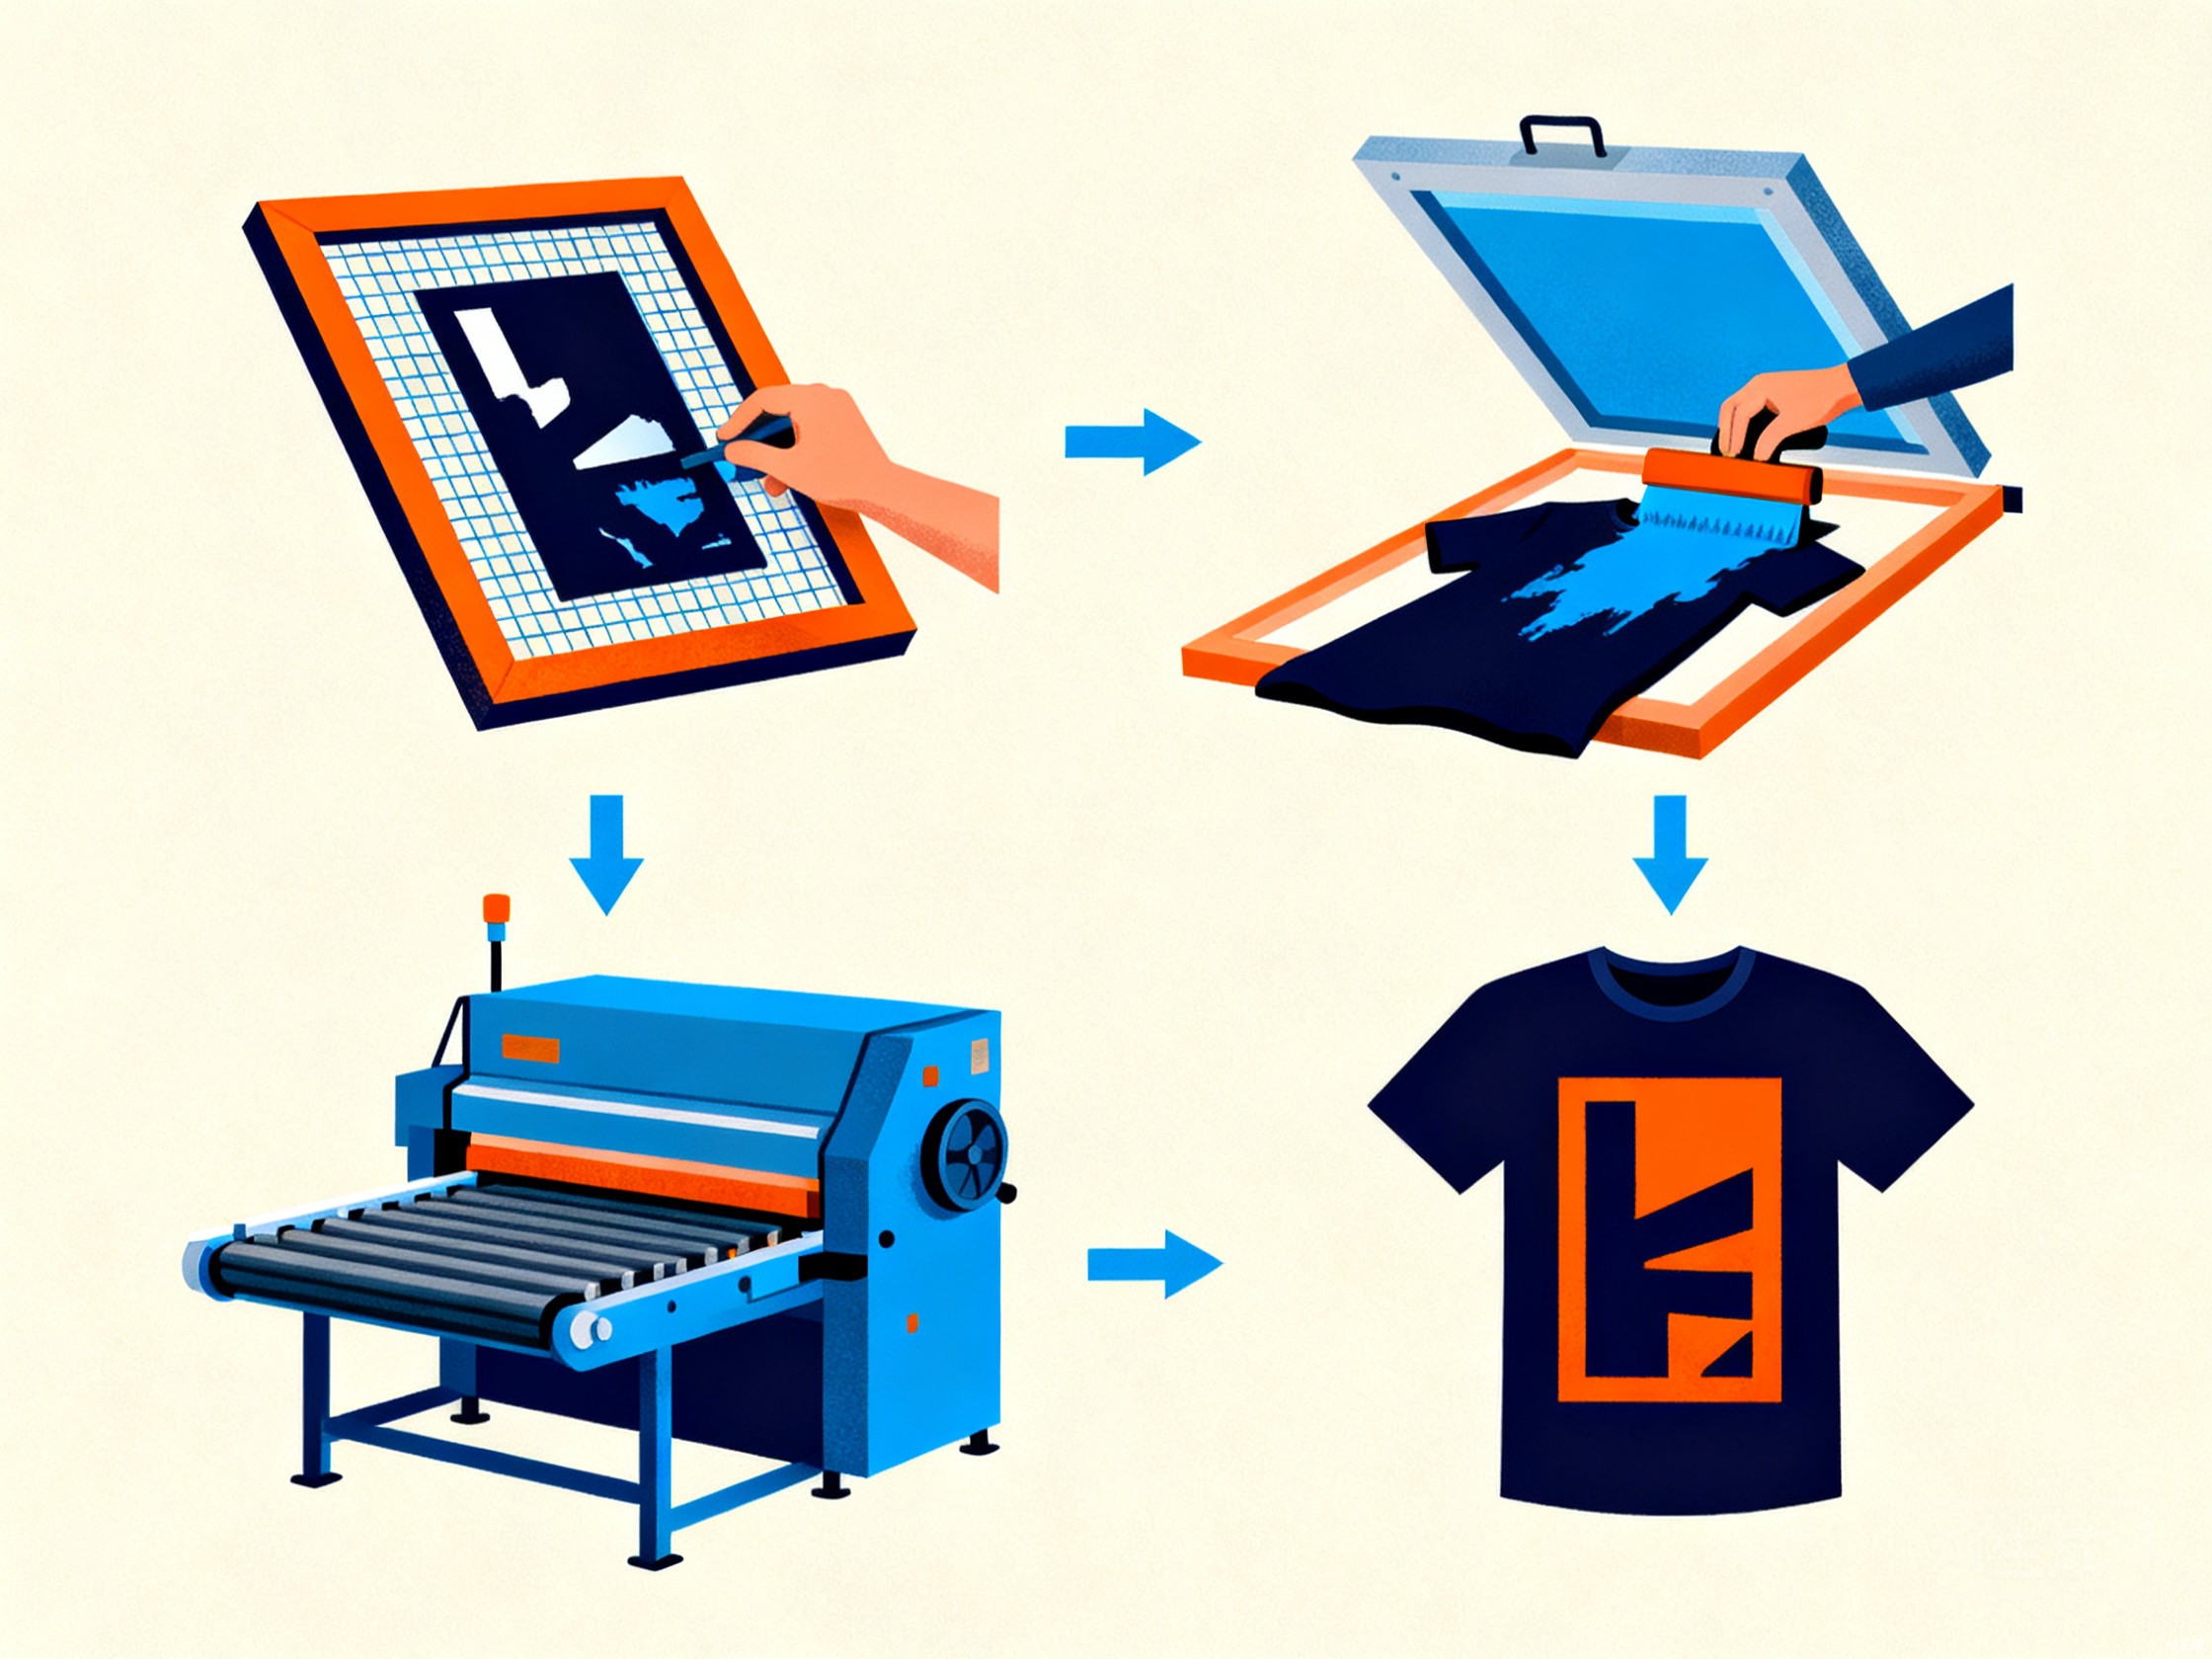
Screen printing (also called silk screen or serigraphy) pushes ink through a fine mesh stencil onto fabric. Each color in the design needs its own screen, which is why screen printing is most cost-effective for bold 1–4 color designs on cotton. Plastisol ink is the industry standard: it sits slightly on top of the fabric, gives vivid opaque color on dark shirts and lasts through years of wear.
When screen printing wins
- 1–4 spot color designs on cotton or poly-cotton blends
- Dark fabric where opacity matters (no see-through)
- Larger runs (100+ pieces) where per-piece price drops sharply
- Specialty inks: metallic gold/silver, glow-in-the-dark, puff, high-density
When screen printing is the wrong choice
- Full-color photographic designs — each color = a new screen, 6+ colors gets expensive
- Tiny runs under 25 pieces — setup cost amortizes badly
- Designs that change every order — we have to remake screens each time
Read more about the technical details in the Wikipedia entry on screen printing.
What is embroidery?
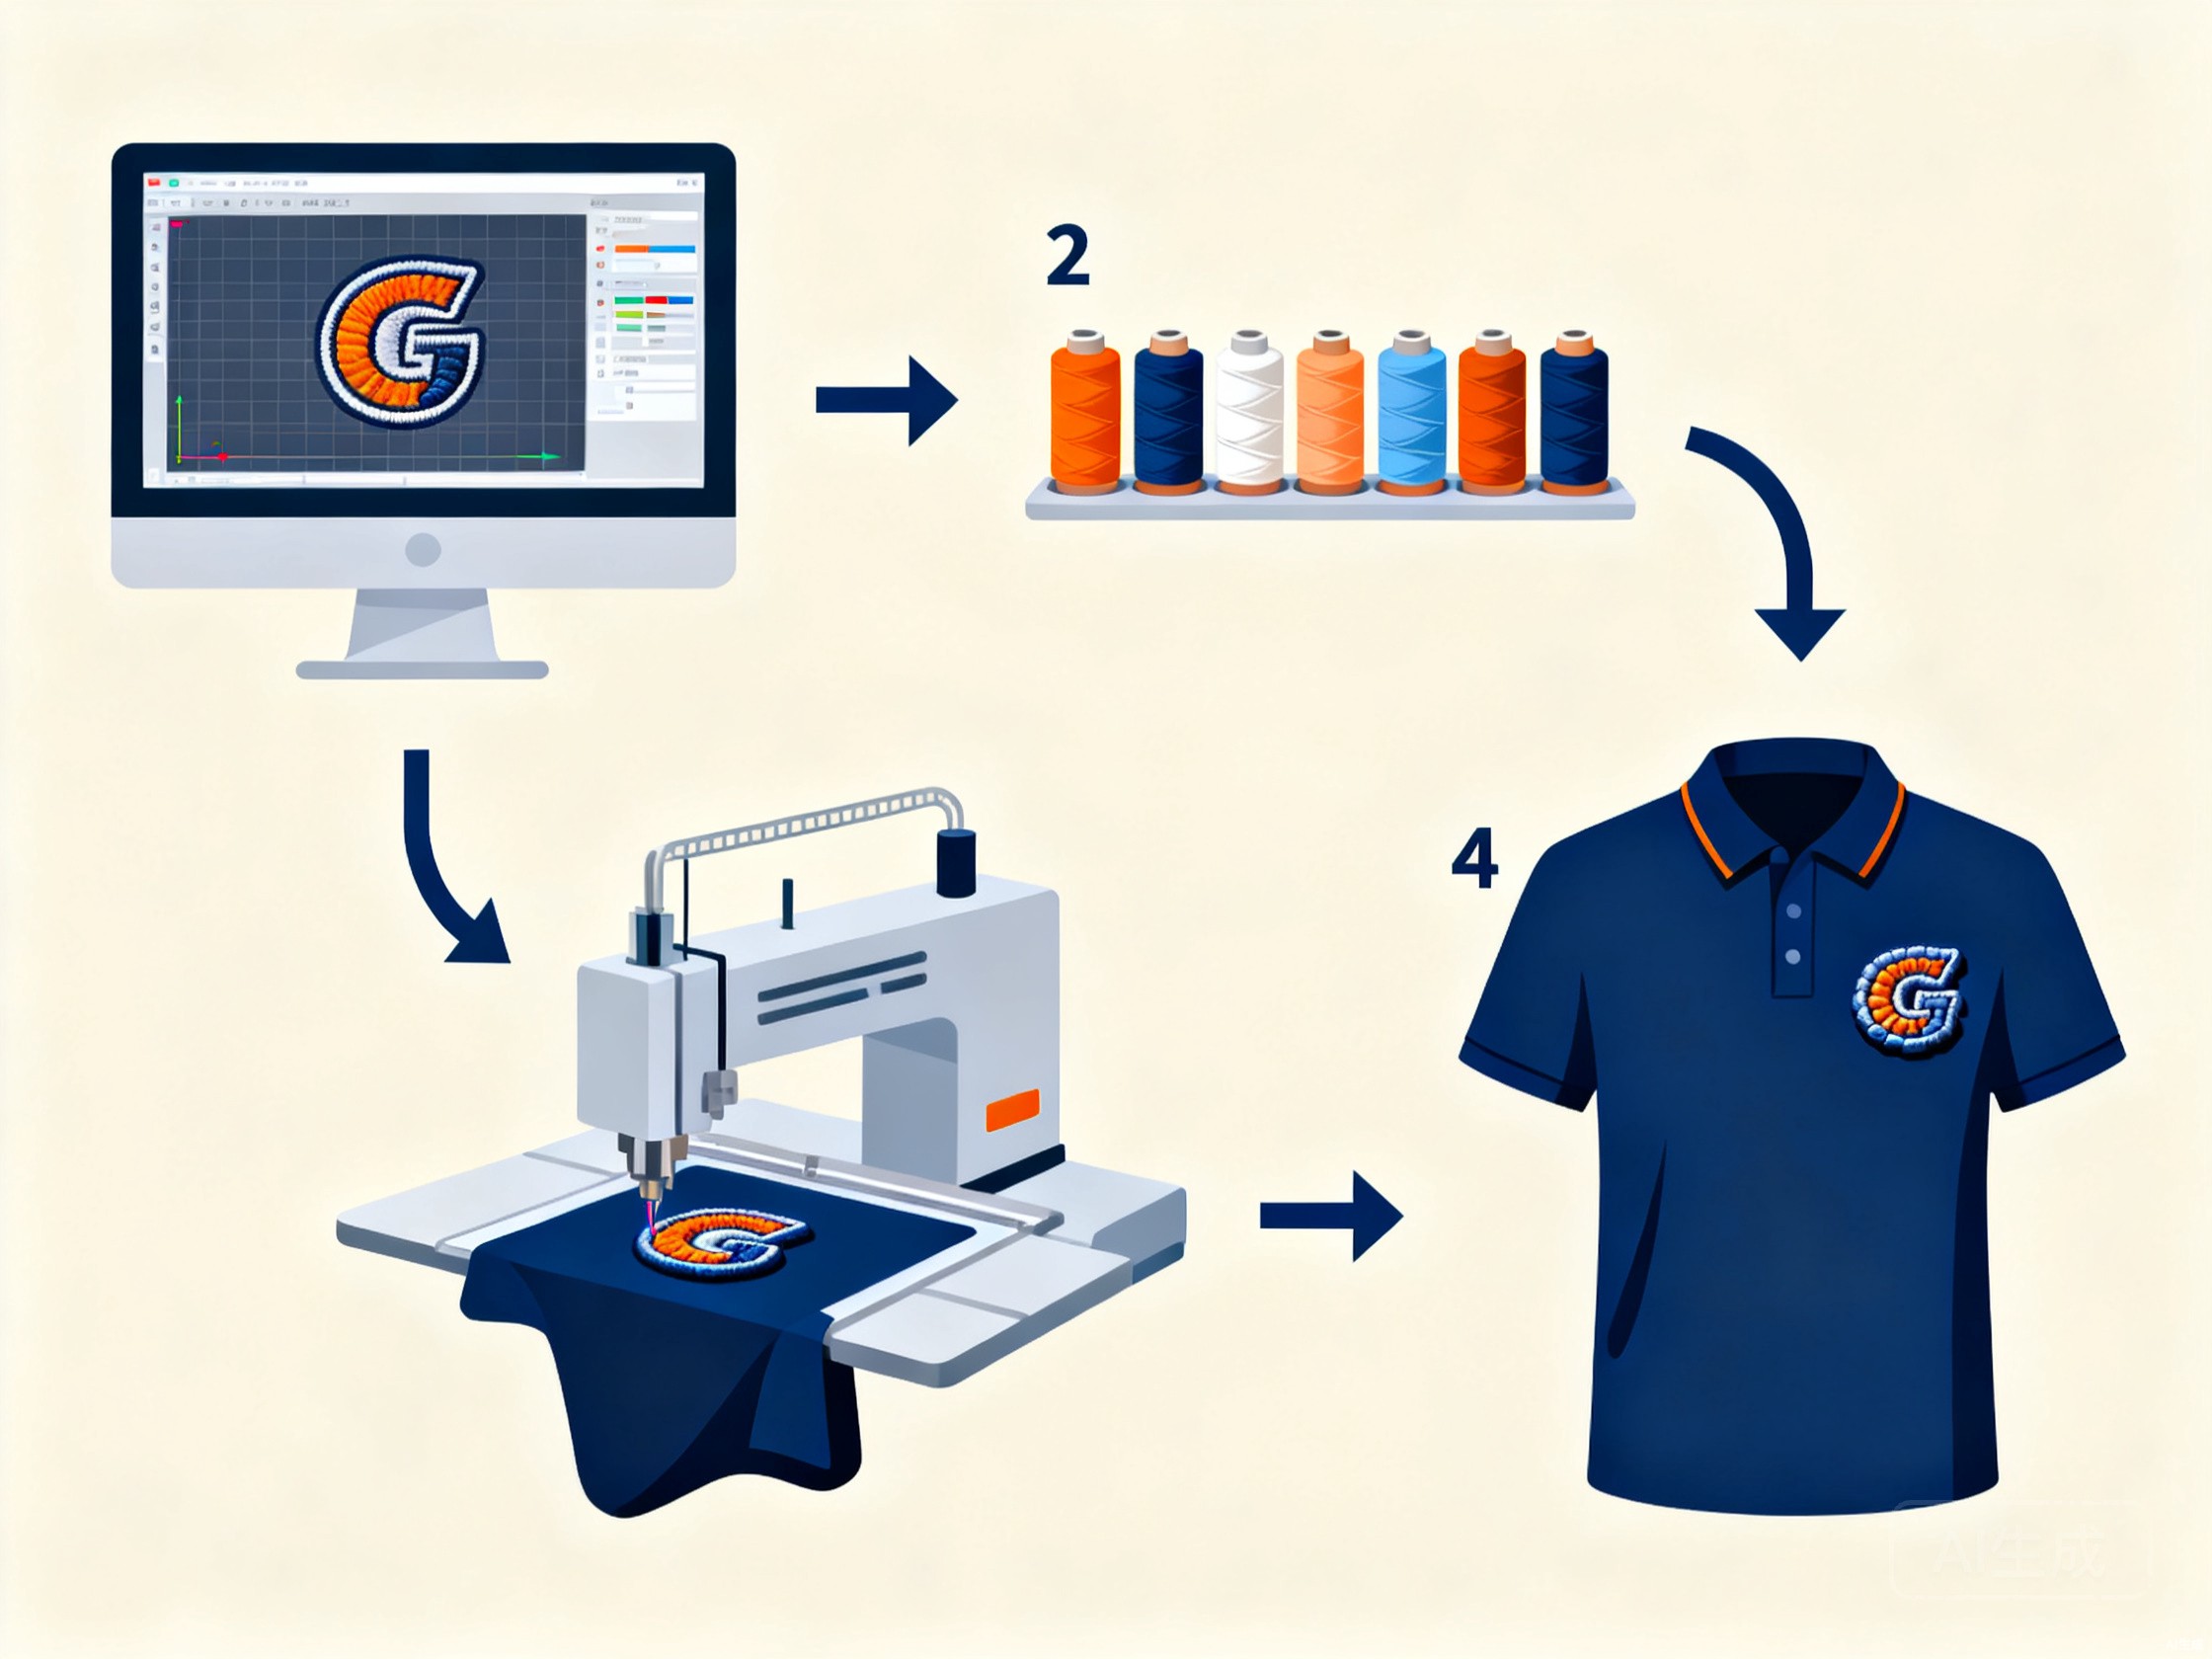
Embroidery is not printing — it stitches thread into the fabric with an industrial embroidery machine. The logo first goes through a one-time digitization step that converts the artwork into a stitch file (.DST or .EMB). The file then drives the machine, which can hold up to 12 thread colors and stitch thousands of stitches per minute.
When embroidery wins
- Corporate logos on polos, dress shirts, jackets, caps and workwear
- Premium retail brands that want a 3D tactile logo
- Durability is critical — thread outlasts the garment
- No setup per garment color (digitizing fee is one-time per logo)
When embroidery is the wrong choice
- Photographic or gradient artwork — embroidery cannot reproduce those
- Very small text below 5 mm — letters become unreadable in thread
- Lightweight thin fabrics (e.g. 110 gsm single-jersey) that pucker under stitching
Background on the craft is on the embroidery Wikipedia entry.
Other methods: DTG, heat transfer & vinyl
Beyond the big three, three more methods are worth knowing about for small orders and special finishes:
DTG (Direct-to-Garment)
DTG is essentially an inkjet printer for t-shirts. It sprays water-based ink directly into cotton fibers. Great for one-off samples and full-color designs on 100% cotton. Downside: slower per piece, slightly less durable than sublimation or plastisol screen printing.
Heat transfer / digital transfer
A design is printed on special paper, then heat-pressed onto the garment. Used for small runs of complex designs, names & numbers on sportswear, and reflective safety garments. Sits on top of the fabric like a thin film.
Vinyl (HTV)
Pre-colored vinyl is cut with a plotter and heat-pressed. Best for single-color text, simple shapes and small runs of sports jerseys with names and numbers.
For a broader overview of apparel decoration in general, the sublimation phase transition article explains the chemistry.
Head-to-head comparison table
Here is everything side-by-side so you can pick fast.
| Factor | Sublimation | Screen printing | Embroidery | DTG |
|---|---|---|---|---|
| Best fabric | Polyester / poly blend | 100% cotton | Polo, twill, oxford | 100% cotton |
| Color count | Unlimited (CMYK) | 1–6 spot colors | Up to 12 thread colors | Unlimited (CMYK) |
| Photo / gradients | Excellent | Limited (halftones only) | Not possible | Excellent |
| Dark fabric | Possible with white underbase | Excellent | Excellent | Excellent (with white underbase) |
| Hand feel | Zero texture (in fabric) | Thin layer over fabric | Raised 3D texture | Soft, ink in fabric |
| Durability (50 washes) | Excellent | Very good | Excellent | Good (may fade) |
| Setup cost | None | ~$30–$50 per color (screen) | ~$20–$50 digitizing (one-time) | None |
| Best MOQ | 25 pcs | 50–100 pcs | 25 pcs | 1–10 pcs |
| Unit price (100 pcs) | $4–$8 | $2–$4 | $3–$7 | $8–$14 |
| Lead time at OEM T-Shirts | 45 days | 45 days | 45 days | 45 days |
How to choose the right method for your project
Walk through this 4-question decision guide before sending your artwork:
① What fabric is the blank?
Cotton → screen print or DTG. Polyester → sublimation. Polo/twill/canvas → embroidery. This single question eliminates two of the three options.
② Is your artwork photo or vector?
Photographic, gradients, skin tones → sublimation or DTG. Flat colors, logos, text → screen print or embroidery.
③ How many pieces?
Under 25 pcs → DTG, vinyl, or sublimation. 50+ pcs → screen printing becomes cheapest. Embroidery is roughly flat in price across quantities.
④ What’s the use case?
Retail re-sell → sublimation or DTG. Corporate uniform → embroidery. Sports team → screen print + numbers. Promotional giveaway → screen print.
Still unsure? Our team has produced over 10,000 custom t-shirt orders from our Yiwu factory. Send us your artwork and a short brief and we will recommend the most cost-effective method within 12 hours.
MOQ, pricing & lead time at OEM T-Shirts
Here is what to expect when you place an order with us:
- MOQ: 25 pieces per design across sublimation, screen printing and embroidery. Mixed sizes and colors in one design count toward the 25-piece minimum.
- Sample lead time: 5–7 days (DHL/FedEx shipping extra, refundable on bulk order).
- Bulk lead time: about 45 days after payment and PP sample approval, broken down as: 3–5 days for revised sample if needed, 30–35 days for bulk production, 7–10 days for QC and export packing.
- Shipping terms: EXW, FOB, CIF, DDP available — see our shipping & logistics page for port options.
- Payment: 30% T/T deposit + 70% balance before shipment. PayPal accepted for samples under $1,000.
For an overview of how custom apparel programs are structured by retail brands, see Shopify’s clothing line guide and Printful’s custom t-shirt comparison.
Frequently asked questions
Which printing method is cheapest for 100 t-shirts?
For 100 cotton t-shirts with a 1–2 color design, screen printing is usually the cheapest at roughly $2–$4 per piece. Sublimation is cheaper per piece only on white polyester blanks and full-color designs. Embroidery is the most expensive, typically $3–$7 per piece.
Can you sublimate on 100% cotton t-shirts?
Pure sublimation requires polyester — the dye bonds with the synthetic polymer. For cotton you can use sublimation with a polyester coating transfer, but the result is less soft and less durable. For all-cotton blanks, screen printing or DTG is the better fit.
What is the minimum order quantity (MOQ) for custom t-shirts?
OEM T-Shirts offers MOQ 25 pieces per design for sublimation, screen printing and embroidery. Sublimation MOQ can drop to 10 pieces for repeat orders. Embroidery MOQ starts at 25 pieces because each logo requires a digitizing fee on the first order.
Which method is most durable after 50 washes?
Embroidery is the most durable — the threads themselves do not fade. Sublimation becomes part of the fabric and outlasts 50+ washes without cracking. Plastisol screen printing lasts long but can crack after heavy use. DTG is the least durable of the four after repeated washing.
How long does production take for custom t-shirts?
OEM T-Shirts standard production time is about 45 days after payment and PP sample approval: 3–5 days for sampling, 30–35 days for bulk production, 7–10 days for QC and export packing. Sample-only orders can ship in 5–7 days via DHL.
Can I mix screen print and embroidery on the same t-shirt?
Yes, mixed decoration is very common — for example a large screen-printed graphic on the body plus an embroidered logo on the chest or sleeve. OEM T-Shirts supports mixed decoration in one production run; the embroidery digitizing fee is one-time per logo.
By Ramon Wang — Production Manager, OEM T-Shirts. 12 years in custom apparel manufacturing from our Yiwu factory.
